Practical Performance
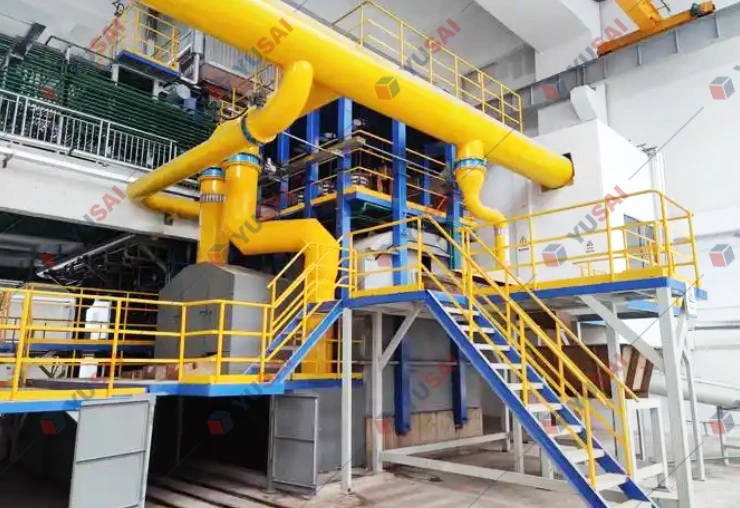
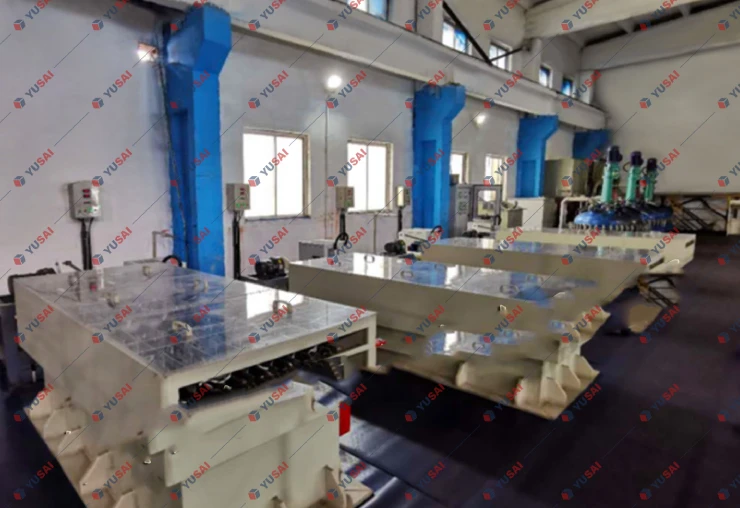
A domestic company has adopted our company’s silver electrolytic cell for high-current-density silver electrolysis production. Through this trial run, the following advantages have been summarized: environmentally friendly, labor-saving, time-saving, energy-efficient, and ensuring the stability of technical parameters. These advantages are manifested in the following aspects:
a. Improved On-Site Working Environment
The silver electrolysis equipment uses a refrigerator to cool the electrolyte. When the electrolyzer is in operation, the refrigerator temperature is set to 40°C. When the electrolyte temperature reaches 40°C, the refrigerator automatically starts to cool the electrolyte, and when the temperature drops below 40°C, the refrigerator automatically stops. Electrolysis at a reasonable temperature prevents electrolyte volatilization, eliminating the presence of acid gas in the workshop. Compared to the old workshop, the working environment has significantly improved.
b. Fast Electrolysis Speed and Increased Production
The electrolysis speed is fast, with a conventional silver electrolysis current density of 300 A/m² (while our silver electrolysis current density reaches 750 A/m²). The current density is 2-3 times that of conventional silver electrolyzers. With equipment of the same size, production capacity is significantly increased. For the same production capacity, less workshop area is required. This effectively increases the equipment’s production capacity (by 2-3 times). With a current operating current of 1500 A, the actual production is 55 Kg/hour, reaching the designed capacity of 1000 Kg/day. This significantly reduces the amount of silver tied up and lost during production, substantially reducing the company’s working capital and financial costs.
c. Convenient Worker Operation, Time-Saving, and Labor-Saving
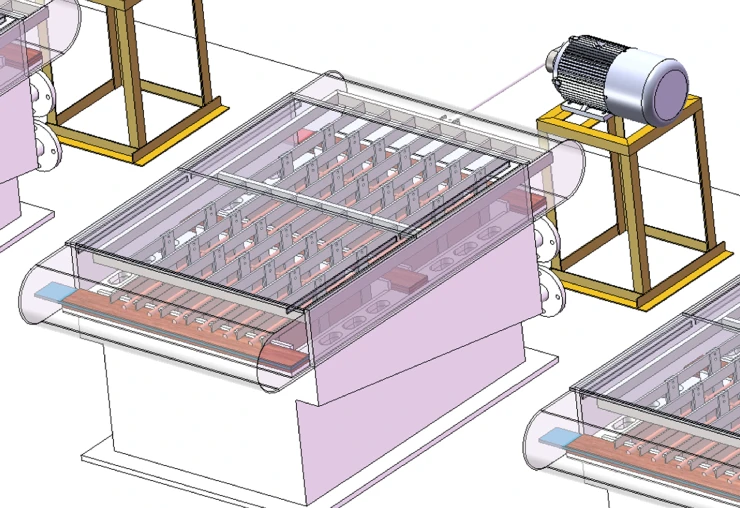
- A mechanized conveyor belt is used for silver powder discharge. The silver powder deposited on the cathode is scraped onto the mechanical conveyor belt at the bottom of the cell, transported out of the electrolyzer through a sloped structure at the front of the cell, and directly falls into a vehicle for silver powder transportation, which is then sent for washing and ingot casting. This reduces worker labor intensity.
- An automatic stirring device is used, automatically scraping off the silver powder produced on the cathode plate without manual scraping, avoiding short circuits between the cathode and anode. This improves the reliability of electrolyzer operation. Originally, production had to be stopped once a month for cell bottom cleaning, but now continuous production can last nearly 7 months without shutdown for cleaning. This also reduces worker labor intensity.
d. Energy Conservation
- The silver electrolyzer is equipped with an automatic stirring device, avoiding short circuits between the anode and cathode. There is no silver powder in the anode bag, saving a significant amount of nitric acid when treating anode slime. According to current statistics, the daily nitric acid consumption for boiling anode slime has decreased from 400 Kg/day to 300 Kg/day.
- With a daily reduction in nitric acid consumption of 100 Kg, 36.5 Kg less nitrogen oxides are produced daily. Based on previous detection data with an air volume of 7000 m³/hour, the nitrogen oxide content has decreased by 1738 mg/m³, reducing nitrogen oxide emissions and saving subsequent treatment costs.
Improve the Operational Stability of Electrolytic Cells
The new-type silver electrolyzer adopts a new electrolyte circulation method, changing the circulation flow direction of the electrolyte in the electrolyzer to a parallel flow with the arrangement of the anode and cathode, entering from the bottom and exiting from the top. This effectively reduces concentration polarization between the anode and cathode, significantly increasing the current density of electrolysis production while ensuring that the silver powder quality meets the national standard for No. 1 silver, and reducing the silver ion concentration in the electrolyte.
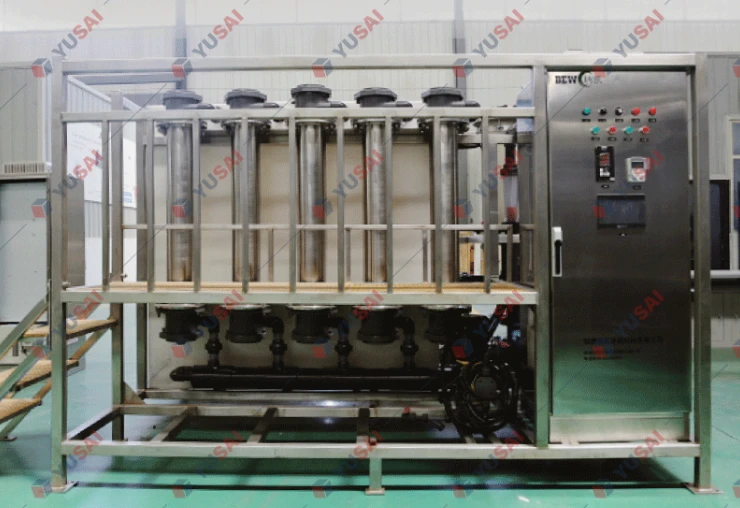
Advantages of Yusai Silver Electrolyzers for Material Discharge Under High Current Density
- Enclosed electrolyzer with side fume extraction.
- Daily production per cell: 100 Kg with 600 liters of electrolyte held up; 200 Kg with 1000 liters; 300 Kg with 1500 liters.
- Small equipment footprint.
- Single-cell electrolysis for different anodes, ensuring no cross-contamination of produced silver powder.